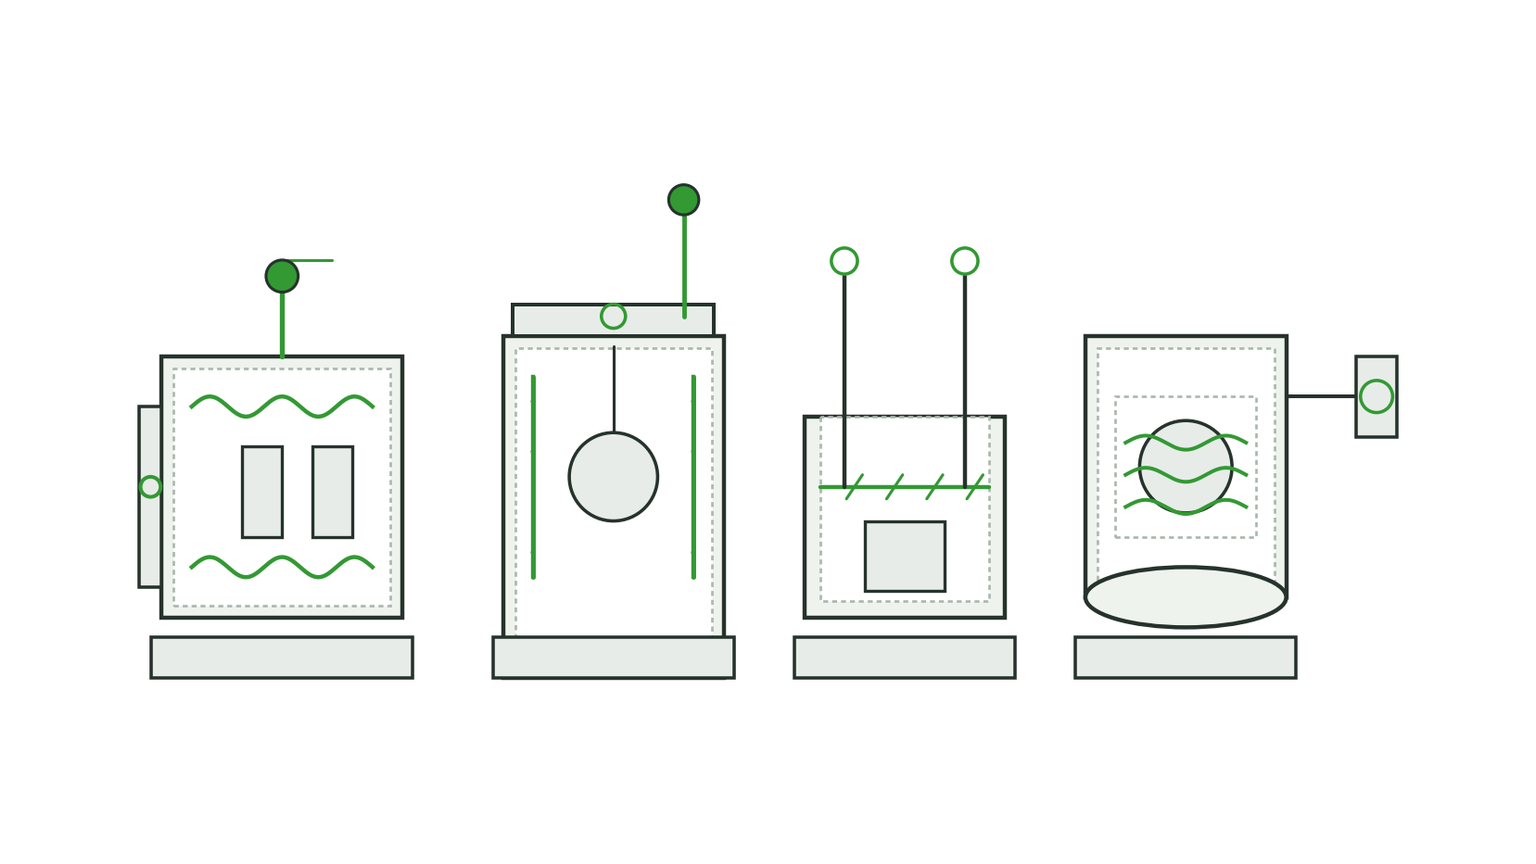
Furnace Types
Batch furnace (Batch Furnaces)
Box furnace / box furnace (Box / Chamber)
The most common batch furnace type, broad specification coverage, suitable for annealing, normalizing, stress relief, tempering, solution treatment and aging.
Advantages:High heat capacity, excellent temperature stability, life 15–25 year, resistant to mechanical damage, usable up to 1700°C.
Disadvantages:Slow heat-up/cool-down, high energy consumption.
Advantages:Low heat capacity, fast heating and cooling, energy saving 20–40%.
Disadvantages:Low mechanical strength, high air velocity causes fiber spalling, relatively short service life.
Pit furnace (Pit)
Vertical arrangement, suitable for hanging long-shaft workpieces for heating, reduce distortion; convenient loading with the furnace cover open, often used for long bars, lead screw, annealing and carburizing of cylindrical parts.
Bell furnace (Bell)
Inner hood / outer-hood structure, bulk material heating, good protective-atmosphere circulation, suitable for coils, annealing of wire coils; multiple positions can rotate, high throughput.
Sealed-quench furnace (Sealed Quench)
Carburizing / quenching / integrated tempering, in-furnace quench oil tank or salt bath, workpiece transfer without oxidation. Suitable for gears, bearing, batch carburizing and quenching of fasteners, etc..
Vacuum furnace (Vacuum)
Heating under vacuum or low-pressure atmosphere, no oxidation or decarburization; hot-wall / cold-wall structure; suitable for tooling, stainless steel, titanium alloy, bright heat treatment of superalloys and vacuum brazing.
Salt-bath furnace (Salt Bath)
Barium chloride / sodium chloride / nitrate medium, fast heat-up, uniform temperature, flexible local heating; suitable for high-speed-steel quenching, austempering, marquenching.
Fluidized-bed furnace (Fluidised Bed)
Airflow suspends particles, heat-transfer coefficient close to salt bath with no pollution; suitable for batch heating of small parts and continuous-furnace preheat zones.
Continuous furnace (Continuous Furnaces)
| Furnace type | Conveying method | Suitable workpieces | Typical temperature |
|---|---|---|---|
| Mesh-belt furnace | Metal mesh belt | Small fasteners, bearing, standard parts | 400–1000°C |
| Pusher furnace | Tray push-feeding | Medium-batch gears, shafts | 700–1050°C |
| Roller-hearth furnace | Heat-resistant roller drive | Plate, bars, steel pipe | 500–1100°C |
| Rotary furnace (Retort) | Rotary cylinder | Small parts, powder | 400–950°C |
| Walking-beam furnace | Walking-beam mechanism | Bloom, slab, steel pipe | 600–1250°C |
Kiln (Kilns)
Tunnel kiln ( continuous firing), rotary kiln ( powder material / aggregate), shuttle kiln ( intermittent, movable trolley). Used for ceramic firing, refractory calcination, lime and molding-sand treatment.
Oven (Ovens)
Special-process equipment
Selection points
- Batch size and takt time decide batch or continuous type;
- Max operating temperature and lining grade determine capital cost and energy use;
- Atmosphere requirement ( oxidation / protection / carburizing) determines furnace sealing and auxiliary systems;
- Shop height and charging method ( crane / trolley / roller table) limits furnace geometry.
Heat-Treatment Process Reference
Core process
Non-ferrous alloy
- Aluminum alloy:T6( solution treatment 525°C + artificial aging 175°C/8h) is a typical condition; annealing O condition softening.
- Copper and brass:Stress-relief annealing 200–300°C; prevention of brass season cracking ( stress relief + slow cool).
Metallurgical basis
TTT the curve describes isothermal transformation (C curve nose 550°C nearby),CCT the curve describes continuous cooling transformation; critical cooling rate Vc determines quench success. Austenite grain size and hardenability (Jominy) is central to grade selection.
Steel-grade database
This siteMaterial databaseCollects critical temperatures of common steel grades, quenchant, tempering curves and isothermal-transformation data, searchable by steel grade.
Process-design principles
- Hardness-toughness trade-off: for each rise in tempering temperature of about 25°C, hardness drops 2–4 HRC;
- Quench-distortion control: pre-cool, marquenching / austempering, press quenching;
- Decarburization and oxidation protection: protective atmosphere, vacuum, salt bath or coating;
- Case-depth profile should transition gradually, avoid carbide network.
Atmosphere Selection
Flammable atmosphere
Endothermic atmosphere (Endothermic,RX)
Key process:Carburizing carrier gas ( blended with enrichment gas), carbonitriding, recarburization.Furnace effect:Carbon balance at the steel surface is controlled by carbon potential;CO toxic, explosion-proof.
Exothermic atmosphere (Exothermic,NX)
Oxygen-lean combustion products (N₂ predominant + CO₂/H₂O), used for annealing, positive carbon, copper-brazing protection; low preparation cost, dew-point control removes water.
Dissociated-ammonia atmosphere (AX)
2NH₃ → N₂ + 3H₂(75/25), catalytic cracking; used for stainless-steel annealing, powder metallurgy, bright treatment of low-carbon steel.
Nitrogen-based atmosphere (N₂ + methanol / enrichment gas)
Liquid nitrogen /PSA nitrogen + cracked methanol, flexible ratio, gradually replaces endothermic atmosphere.
Hydrogen (H₂)
Strongly reducing protective atmosphere, used for stainless-steel annealing, powder metallurgy and in-furnace brazing; low density, after a leak it accumulates toward the furnace top, lower flammable limit 4%, explosion-proof design is mandatory ( flame arrester, double-wall pipe, hydrogen-monitor interlock) and pre-ignition purge.
Non-flammable atmosphere
Nitrogen (N₂)
Inert protection, tempering, anti-oxidation annealing; oxygen content controllable <10ppm( high purity).
Argon (Ar)
Vacuum-furnace backfill, protection of titanium and superalloys; density greater than air, good displacement.
Vacuum and low pressure
Vacuum (10⁻¹–10⁻⁴ Pa) or low-pressure inert atmosphere for oxidation-free heating and degassing, suitable for titanium alloys, bright annealing of superalloys and stainless steel; see the vacuum-system topic.
Safety boundary
Carbon-potential control
Use oxygen probe (ZrO₂) oxygen measurement → convert to carbon potential;CO/CO₂ infrared-analysis correction; dew-point meter measures moisture. Target carbon potential 0.9–1.1%( carburizing), deviation ±0.05%.
Quench Media
1. Quenching Theory and the Three Stages
Quenching is steel part cooling from austenitising temperature fast, turning face-centred cubic austenite into body-centred tetragonal martensite – diffusionless shear-type transformation –Cooling rate is the key.。
Critical Temperatures
| Parameters | Typical value |
|---|---|
| Austenitising temperature (carbon steel) | 800-870°C |
| Austenitising temperature (tool steel) | 1000-1220°C |
| Ms martensite start (Ms) (typical) | 200-350°C |
| End of Mf martensite (typical) | 50-150°C |
| Pearlite nose (CCT) | 500-600°C |
| Bainite nose (CCT) | 300-400°C |
Critical Cooling Rate (for a Fully Martensitic Structure)
| Steel grade | Critical cooling rate |
|---|---|
| Plain carbon steel 1045 | >200°C/s |
| Low alloy 4140 | About 30°C/s |
| Medium Alloy 4340 | About 8°C/s |
| Tool steel H13 | About 3°C/s |
| High-speed steel M2 | <1°C/s |
Three Stages of Liquid Quenching
Duration: 2-10 seconds in oil (with mixing).
Overwrites pearlite between bainite nose and bainite nose on CCT charts.
This phase is still important to ensure even cooling.
CCT and Hardenability
- Alloy elements (cr, Mo, Ni, Mn) enable pearlite/bainite nose to move right (longer time) to lower critical cooling rate
- Carbon content effect Ms temperature: The higher the carbon, the lower the Ms
- The thicker the hardenability, the better.
- TTT (temperature) maps are used for temperature maintenance;Quenching, please use CCT
Ms(°C) = 539 − 423C − 30.4Mn − 17.7Ni − 12.1Cr − 7.5Mo − 7.5Si
EN19(4140) Example: C=0.40、Mn=0.80、Cr=1.0、Mo=0.20 → Ms = 539 − 169 − 24 − 12.1 − 1.5 = 332°C
2. Quench Severity (Grossmann H-Value)
H-value quantitative medium relative to ideal quenching (H = <unk>) heat-replacement capacity, H is bigger and more intense. To project hardness distribution by Jominy data.
| Media and Status | H (in-1) | Relative intensity |
|---|---|---|
| Still Air | 0.02 | Very weak. |
| Mobile air (frozen) | 0.05 | Weak |
| Nitrogen 2 bar (cycle) | 0.04-0.06 | Weak |
| Nitrogen 6 bar | 0.08-0.12 | Weak |
| Nitrogen 10 bar | 0.15-0.20 | Medium |
| Nitrogen 20 bar | 0.25-0.35 | Medium |
| Helium 6 bar | 0.20-0.30 | Medium |
| Helium 20 bar | 0.50-0.70 | Significant |
| Still oil (40-80°C) | 0.25-0.35 | Medium |
| Trigger oil (40-80°C) | 0.35-0.70 | Significant |
| Still Water (20-30°C) | 1.0 | High |
| Smash the water. | 1.5-4.0 | High |
| Salt water 5-10% Nacl (mixed) | 2.0-5.0 | Very strong. |
Jominy Equivalence: The range of Jominy with a given H value corresponding to the diameter of the bar can be traced by Lamont figure. Example: <unk>50mm bar in mixed oil (H=0.50) with a heart equivalent Jominy distance of approximately 11mm, surface about 5mm – and thus hardness is predicted from the open Jominy curve.
3. Quench Medium Selection Matrix
| Steel grade Category | Typical | Preferred Medium | Alternative | Description |
|---|---|---|---|---|
| Low alloy structure steel | 4140, 4340, EN19, EN24 | Oil (standard/fast) | PAG 10-15% | (b) Oils selected from the thick side; Thread wall distortion sensitiveware polymer |
| Carbon steel (<0.60 C) | 1045, EN8, EN3 | Water or salt water | PAG 5-10% | Hardenability Low-needs intensive quenching; The complex shape is cracking risk. |
| Carbon steel (>0.6%C) | 1080, 1095, EN42, EN44 | Oil (fast/standard) | PAG 15-20% | Water quenching excessive cracking risk; oil quenching + tempering for standard |
| Hot die steel. | H11, H13, H21 | Empty or gas quenching (N2 <unk>6 bar) | Oil (classification) | Empty steel grade; vacuum furnace gas quenching for standard |
| Cold die steel | D2, D3, A2, O1 | Air Cold (A)/Oil (O/D) | Gas quenching N₂ 6-10 bar | D2 Vacuum; O1 oil quenching; D3 oil quenching or salt bath |
| High-speed steel | M2, M42, T1, T15 | Gas quenching (N2 or He <unk>6 bar) | Salt bath, oil (grade) | Vacuum +gas quenching is standard; Salt bath austempering for traditional processes |
| Martensite stainless steel | 410, 420, 440C | Oil or air-cold | Gas quenching N₂ 6 bar | Hardenability medium; The thin walls are cold. |
| Sediment solid stainless steel | 17-4PH, 15-5PH, 13-8PH | Gas quenching (N2 2-6 bar) or air cold | — | +ageing; critical cooling rate low; Oil avoidance (pollution risk) |
| Nickel high-temperature alloys | Inconel 718, Waspaloy, Mar-M247 | Gas quenching (Ar or N2 2-6 bar) | — | Vacuum + gas quenching only; Active ingredient for Ar |
| Aluminium alloy (ageing enhanced) | 2024, 6061, 7075 | Water (60-80°C) | PAG 5-10% | Quenching immediately after solidification; thin sheet lower distortion with PAG |
4. Oil Quenching
4.1 Classification of Quench Oils
| Level | 800-400°C cooling rate | Maximum cooling rate | Temperature | Typical application |
|---|---|---|---|---|
| Standard (slow speed) | 12-14 s | 60-80°C/s | 40-80°C | Normal quenching, carburising gear, low-alloy steel |
| Medium Speed/ fast | 8-10 s | 90-120°C/s | 40-70°C | Carbon steel, large transects, hardenability requirement high |
| High-speed | 6-8 s | 120-160°C/s | 40-60°C | Plain carbon steel for water quenching fire |
| Austempering oil | Wait till the temperature stays. | Variable | 80-200°C | Ms. Keep rear air cold above and lower distortion; tool steel, precision parts |
4.2 Commercial Oil Specifications
| Products | Vendor | Type | Flash point°C | Fire point°C | 40°C viscosity cSt | Maximum cooling rate°C/s | Temperature°C |
|---|---|---|---|---|---|---|---|
| Houghton G | Quaker Houghton | Standard | 185 | 210 | 20-24 | 70-85 | 40-80 |
| Houghton K | Quaker Houghton | Fast | 170 | 195 | 14-18 | 100-130 | 40-70 |
| Houghton MT-300 | Quaker Houghton | Wait for the temperature. | 250 | 280 | 28-34 | Variable | 120-200 |
| Park AAA | Park Thermal | Standard | 190 | 215 | 21-25 | 75-90 | 40-80 |
| Park 50 (hot oil) | Park Thermal | Fast (hot) | 200 | 225 | 16-20 | 90-110 | 60-120 |
| Park M-50 | Park Thermal | Wait for the temperature. | 260 | 290 | 30-36 | Variable | 120-200 |
4.3 Quench Tank Design and Agitation
| Item | Requirement |
|---|---|
| Oil – workpiece | Minimum 5:1 (L oil: kg workpiece), recommendation 8-10:1 |
| Every temperature. | <20°C |
| Normal work temperature | 40-80°C (standard oil maximum 80°C) |
| Smash | Propellers (most commonly, 0.5-1.5 m/s perflux)/Thrusters (no motion components)/flowers |
| Heat exchanger | Shell tube (50-500 kW, most common)/Board (hard, pre-filter)/external cooler |
| Fire | CO2 Total inundation (1-2 kg/m3, most common); (a) Auto-canner cover (with weights safely closed); Foam systems (large open cans); Spill. |
4.4 Quench Oil Maintenance
| Detect items | Method | Frequency | Watch out. | End of life limit |
|---|---|---|---|---|
| Cooling curve | ISO 9950 (Inconel 600 probe) | Monthly | Maximum cooling rate < New oil 80% | < New oil 60% |
| Flash point | Cleveland open cup (ASTM D92) | Monthly | < 170°C (standard oil) | < 150°C Waste |
| Viscosity | 40°C Sports viscosity (ASTM D445) | Quarterly | Higher than new oil > 30% | > 50% (oxidation damage) |
| Water | Calfeihu (ASTM D6304) | Monthly | >0.03%(300 ppm) | > 0.05% (500 ppm, fire risk) |
| General acid value | ASTM D664 | Quarterly | >0.5 mg KOH/g | >1.0 mg KOH/g |
| Particle | Weight method/ count | Quarterly | >50 mg/L | >100 mg/L filter or replace |
Filter:(b) Continuous by-pass filtering (10-25 μm); Magnetic separators decomposers; Bag filters (5-10 μm); Centrifugal separators decomposed of heavy oil sludge.Main causes of deterioration: Hot cracking decomposition (workpiece surface > 300°C), oxidation (high temperature into air), water pollution (heat exchanger leak/cool/wet workpiece), oil sludge (fragmentation carbon residue + scale/oxide scale).
4.5 Oil Quenching Safety
| Parameters | Typical value |
|---|---|
| Flash point | 170-260°C |
| Flames | 195-290°C |
| Auto-Fire Point | 340-380°C |
| Oil mist self-fired point | About 260°C |
| Maximum Total Work temperature | 80°C (standard)/200°C (temperature) |
Tank fire disposal:1 Alert evacuation 2 Close the lid 3 Start CO2 flood 4Strictly prohibited Water extinguisher <unk>5 Cut the pumps and mix the power <unk>6 advise the fire department (description quench oil fire) <unk>7 to confirm the re-opening of must not before the cooling is extinguished.
5. High-Pressure Gas Quenching (HPGQ)
HPGQ is a vacuum furnace standard quenching mode: high pressure gas is injected into thermal zone, with a high power fan/blower cycle cooling through heat exchanger. No liquid exposure is no vapour-blanket stage, pure convection cooling.
Gas Characteristics
| Gases | Threshold coefficient mW/m K | STP density kg/m3 | Relative cooling capacity | Cost factors |
|---|---|---|---|---|
| Nitrogen N₂ | 26 | 1.25 | 1.0 (baseline) | 1.0× |
| Helium He | 152 | 0.18 | 3.0-4.0× | 8-12× |
| Argon Ar | 18 | 1.78 | 0.6-0.7× | 1.5× |
| Hydrogen H2 | 182 | 0.09 | 4.0-5.0× | 2-3× |
N2 is the main force (more than 80% HPGQ devices); He is six times higher than cooling capacity 3-4, but the cost limits are applied to critical aviation and tool steel; H2 cooling capacity maximum, subject to ATEX level equipment; Ar is used only in a situation where N2 causes nitrogenization (Ti, r alloy).
Gas–Pressure–Cooling Rate Relationship
| Gases | Pressure bar | Approximate cooling rate°C/s | H value in-1 |
|---|---|---|---|
| N₂ | 2 | 5-10 | 0.04-0.06 |
| N₂ | 6 | 15-25 | 0.08-0.12 |
| N₂ | 10 | 25-40 | 0.15-0.20 |
| N₂ | 20 | 40-60 | 0.25-0.35 |
| He | 6 | 40-60 | 0.20-0.30 |
| He | 20 | 80-120 | 0.50-0.70 |
| H₂ | 6 | 50-80 | 0.25-0.40 |
| H₂ | 15 | 100-150 | 0.50-0.80 |
System Design Essentials
- Fan/blower: Electrical 75-300 kW (up to 600 kW for large stoves); (b) Centrifugal or axis flow; (b) Top or bottom load; cooling rate for modular velocity control; Overflow 10-30 m/s
- Heat exchanger: Aqueous copper/ stainless steel wings tube, capacity 200-2000 kW; Water flow 5-50 m3/h (water intake 15-25°C); (b) Outside the gas circulation circuits and hot zones; Decreasing capacity, annually check
- Nozzle:(i) 360° full (circle/ cylinder load standard); Orientation nozzle (platform); (b) Re-flow (increased homogeneity per 30-60 seconds); nozzle – Best distance 50-150 mm; Minimum space 25 mm
6. Polymer Quenching (PAG)
PAG polymers use inverse solubility: dissolved in cold water, distilled in heat workpiece surface to form a controlled cooling barrier; The temperature is reduced to the mist point (approximately 74°C) and the polymer is dissolved and recovered. The cooling intensity is controlled by concentration.
| Concentration | Threshold | Equal to | Typical application |
|---|---|---|---|
| 5-10% | High | Quick to slow water. | Aluminium alloy (2024/6061/7075) solid solubility quenching |
| 10-15% | Medium | Standard to speed oil | Carbon steel and low-alloy steel General quenching |
| 15-20% | Lower | Slow to standard oil | Distortion Sensitive steel part, carburising |
| 20-25% | Low | Gas – Oil clearance | Extreme distortion sensitive, thin wall, spring |
Operating Parameters
| Parameters | Requirement |
|---|---|
| Liquid temperature | 25-40°C (best 30°C) |
| Fog Point | About 74°C (below this temperature polymer redissolved) |
| pH | 8.5 – 9.5 (maintained with microbicides) |
| Smash | Required – recommended 0.3-0.8 m/s |
| Bringing out losses | 1 – 3 per cent per unit (discovery) |
| Refractometer readings | The multiplier (typical 3.5-4.0) should be real concentration |
Commodities: AquaQuench 251 (general steel quenching)/AquaQuench 365 (aluminium solid solution)/Aquatensid N (high performance PAG).Maintenance: Weekly refractometer for concentration; PH to maintain 8.5-9.5 (too low = bacterial breeding); monthly ISO 9950 cooling curve; (a) Refill the tape with concentrate;Prohibited mix different brands PAG(Incompatible polymers can be dissected); annually replaces or cooling curve replaces 20% when deviating from the new liquid.
7. Water and Brine Quenching
Water and salt water provide maximum quench severity (H-Kada 5.0), but distortion cracking risk significant, mainly for low hardenability plain carbon steel, which cannot reach hardness.
| Media | Temperature°C | H value | Maximum cooling rate°C/s |
|---|---|---|---|
| Still Water | 20 | 1.0 | 200-300 |
| Smash the water. | 20 | 1.5-4.0 | 300-600 |
| Hot water. | 60-80 | 0.20-0.40 | 80-150 |
| 5% Nacl salt water | 20 | 2.0-3.0 | 400-700 |
| 10% Nacl salt water | 20 | 3.0-5.0 | 500-900 |
| 10% Naoh alkaline liquid | 20 | 2.0-3.0 | 400-700 |
Temperature control: Water temperature significant affects intensity (20°C heavy, 60°C much more mild); Production needs to be maintained at 20-30°C with cooling towers or plates; <unk>5°C per unit temperature.Added: Nacl 5-10% (most commonly used, corrosion tanks and workpiece); Naoh 3-10% (vapour blanket better control, pH>12); Na2CO3-5-10% (weak base, corrosion light).
Applicability
- Application: Plain carbon steel (1040-1060), Low hardenability, Sensor quenching
- Edge:>0.50%C medium-carbon steel (cracking risk)
- Avoid: Alloy steel (oil quenching sufficient), complex geometry, thin walls, high-carbon steel
8. Salt-Bath Quenching
The salt bath is maintained at controlled temperature et al. To achieve austempering (bainite) and martempering (low distortion martensite). Workpiece impregnated target temperature smelt and kept to transformation completed or even temperature.
| Process | Salt temperature°C | Products | Typical application |
|---|---|---|---|
| Austempering Austempering | 250-400 | Bainite (up/down) | Springs, trucking, hardware, ball iron, high-carbon steel |
| Martempering Martempering | 150-250 (Ms above) | Martensite (low stress) | Gears, bearings, precision tools, distortion sensitive |
| Improved austempering | 300-350 | Bainite + martensite Mixed | Hardness compromise between grinding strength and hardness |
Salt Types
| Salt. | Component | Melting Point°C | Task range°C |
|---|---|---|---|
| AS140 | 50% NaNO₃ / 50% KNO₃ | 140 | 160-550 |
| GS540 | NaNO₃ / KNO₃ / NaNO₂ | 140 | 160-540 |
| Marquench 200 | Modified nitrates | About 130 | 150-250 |
| Park M-Salt | Patented nitrate/nitrate | Approximately 135 | 150-500 |
Austempering vs. Conventional Quench-and-Temper
| Indicators | Contrast |
|---|---|
| Hardness | Bainite 35-55 HRC; QQ0T 58-65 HRC |
| Resilient | 2-3 times the resilience of tempering martensite under hardness |
| Distortion | Mean temperature, significant less than oil quenching |
| Retained austenite | Austempering lower (bainite reaction consumption) |
| Wearyness. | Springs and hardware equal to or better than decomposition |
Salt bath maintenance: <unk>5°C (must mix); Monitoring of carbon, scale/oxide scale, chlorination; Water must is zero (water melted salt will be splattered) workpiece washes immediately after bathing (salt is wet corrosion); Bath time 6-12 months.Environmental protection: Nitrate/nitrate is a oxidation agent (UN 1498/1500) that must be disposed of by a certified waster; Cleaning of water is also dangerous (high nitrate). Many applications have been replaced by HPGQ.
9. Cryogenic Treatment
Many tool steels and high-carbon steel Mf are well below 0°C and room temperature quenching will leave a large amount of austenite. Cryogenic treatment completes the transition by cooling to Mf below.
| Method | Temperature | Media | Keep the time |
|---|---|---|---|
| Cold treatment | −40 ~ −80°C | Dry ice + alcohol or mechanical refrigeration | 1-2 hours |
| Light Cold | −80 ~ −120°C | Mechanical deep cooler or liquid nitrogen temperature control | 2-4 hours |
| Deep Cold (DCT) | −185 ~ −196°C | Fluid nitrogen impregnated or tamponed | 12-36 hours |
Retained Austenite by Steel Grade (As-Quenched)
| Steel grade | Retained austenite |
|---|---|
| D2 | 15-25% |
| M2 | 20-30% |
| 440C | 10-20% |
| 52100 / EN31 | 5-12% |
| Carburising (0.8% C surface) | 15-30% |
Process Sequence
- Austenite and quenching to room temperature (oil, gas or air)
- Quenching after 30 minutes cooled to deep cold temperature (Must not first, tempering)
- Avoid heat shocks by cooling 1-2°C/min
- Target temperature to maintain the set time
- Back to room temperature at 1-2°C/min
- Immediately tempering (tool steel 2 times more)
Main applications: Tool steel (D2/M2/M42) raises hardness and grinding 200-400%; bearing steel (52100) dimensions stabilization; carburising gear (surface retained austenite down to < 5%); Quantities and precision tools; 440C/Surgery equipment to increase corrosivity. Cryogenic treatment (−196°C, 12-36h) can also analyze ultra fine thallium-fe2C carbide, which is more resistant to grinding than a simple austenite conversion (peer review supports 40-30% service life upgrades, depending on steel grade and applications).
10. Quenching Defect Diagnosis
Soft Spots
| Item | Contents |
|---|---|
| Symptom | (a) Locally low hardness (below norm 3-10 HRC) which is common in flats, dents, mobile shield areas; Light stains after nitric acid alcohol is impregnated (pearlite/bainite instead of martensite) |
| Vapour blanket Too long | (b) Increase the mixing speed; Check the propeller turn with the leaf. |
| I don’t have enough mix. | Still to mix; All surface Minimum 0.5 m/s |
| B. Contacts | Improved clothing, increased middle of basket |
| It’s too hot. | Check heat exchanger; Oil > 80°C vapour blanket significant Extension |
| It’s bad oil. | Test cooling curve; maximum cooling rate < 60% new oil is replaced |
| Surface Contamination | Scale/oxide scale or carbon insulation; Improvement of atmosphere or pre-cleaning |
Quench Cracking
| Item | Contents |
|---|---|
| Symptom | Surface visible crack (sometimes only magnets/infiltration visible); typical at angles, key slots, holes, transects; (a) The fragrance of the gold; In short hours (non-tempering phase) after quenching or quenching |
| The medium is too strong. | Aqueous oil or oily polymers; PAG Lower concentration |
| Pointed Geometry | Increase rounded angles (minimal 1.5 mm); Re-engineered Key Slot |
| The cooling is uneven. | Improved mixing homogeneity; HPGQ optimized nozzle layout; Parts to balance flow field. |
| Austenitising temperature is too high | (a) The temperature of the nuclear furnace; Overheated coarse crystals = flaccid |
| Tempering Delay | Tempering in 30 minutes (especially tool steel) |
| Carbon content > 0.60% | Use a more temperate medium; Consider rating or austempering |
| Surface decarburisation | Decarburisation layer transforms first into surface la stress; Use protective atmosphere |
Distortion
| Type | Description |
|---|---|
| Dimensions Change | Austenite martensite volume increase 1-4% (even) |
| Shape Change | Distortion or temperature gradient leads to warp |
| Residual stress | Locked during processing stress Release (Runback) |
| The cooling is uneven. | Improve mixing, nozzle layout (HPGQ) or parts orientation |
Comments
No comments yet. Feel free to ask your model-selection or technical questions; we will reply after review.
Comments are closed on this page.